Tempering Powder Metallurgy Steels
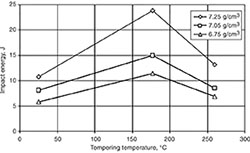
Usually, powder metallurgy steel parts having a density greater than 6.7 g/cm3 (0.242 lb/in.3) should be tempered after hardening. Recommended tempering temperatures for PM parts range from 150 to 200°C (300 to 390°F) with 175°C (350°F) being common. The effect of tempering temperature on impact properties is shown in the graph for FL-4205 at various densities.
Tempering above 200°C results in improved toughness and fatigue properties of the hardened part, while making a compromise in tensile strength and impact resistance. However, when tempering at temperatures higher than 200°C, care should be exercised as entrapped oil can ignite.
Volume 4D, Heat Treating of Irons and Steels -> Heat Treating of Carbon and Low-Alloy Steels -> Heat Treatment of Powder Metallurgy Steels -> Quenching and tempering