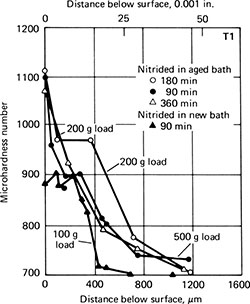
The graph shows the effect of bath conditions and immersion time on hardness gradients in Type T1 high-speed tool steel.
It compares the hardness gradients obtained on specimens of T1 high-speed steel nitrided at 565°C (1050°C) for 90 minutes in a new bath and for various lengths of time in an aged bath. Nitriding of decarburized high-speed steel tools should be avoided because it results in a brittle surface condition. For those surfaces that have been softened from grinding, nitriding is frequently employed as an offsetting corrective measure.
Volume 4D, Heat Treating of Irons and Steels ⇒ Tool Steels ⇒ Heat Treating of High-Speed Tool Steels ⇒ Recommended Heat-Treating Procedures