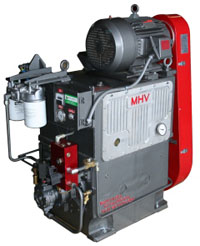
Metallurgical High Vacuum, Fennville, Mich., displays its Survivor pumps in Booth #1639 at the ASM Heat Treating Expo. They incorporate multiple oil filters that extend the life of the pump by removing particles and acid that are harmful. This design extends pump life and increases the return on investment significantly. They use a proven oil-sealed rotary piston design for excellent reliability even in demanding operating conditions.
Their pressurized oil lubrication increases pump life significantly by half- micron rated filters that clean the oil of particulates and acids. Clean oil is forced into the critical hinge bar/piston slide tang interface. The eccentric bearing bands are also pressure lubricated. This design reduces the cost of ownership over the life of the pump, and helps to reduce periodic maintenance. The heavy-duty roller bearing design on main shaft extends life.
The exhibit will also feature rebuilt vacuum pumps which can include the filtration option for tough heat treating applications. MHV rebuilt pumps have become the standard for many customers requiring all-new pumping capacity. “Once they get a pump from MHV, they can see the high quality that our American-made company delivers. They get a pump that looks like new and runs even better. We have customers that can go anywhere for their pump rebuilding, but they come back to MHV because of our quality and service,” notes Geoff Humberstone.