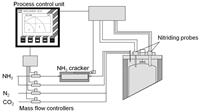
Modern gas nitriding and nitrocarburizing furnaces are equipped with sensor systems and a process control unit that allow the measurement and automatic control of the nitriding potential (KN). The figure shows an example of how the process control can be carried out.
Defined amounts of ammonia, nitrogen, and—for nitrocarburizing processes—carbon dioxide, can be chosen for each step in the program and fed into the furnace via mass flow controllers. The gas composition in the retort is measured via a nitriding probe. For the measurement of nitrocarburizing processes two different probes are needed. The control unit calculates the nitriding potential according to the measured values and controls the mass flow of ammonia to meet the requested set point of KN. During the nitriding process the gasifying amount of ammonia can just be reduced to a certain limit. To keep the KN value low, therefore, precracked ammonia must be added. It must be mentioned that there are some more simple control systems available, which also produce good results.
For more information, click on the link below (subscription required). Then scroll to Figure 25. R Schneider; R. Mesquita; W Schützenhöfer, Distortion in Tool Steels, ASM International, 2014 https://doi.org/10.31399/asm.hb.v04d.a0005958