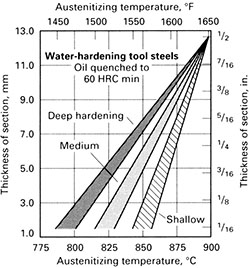
Austenitizing temperatures for water-hardening tool steels normally vary from 1400 to 1550°F. Higher temperatures are sometimes used for special purposes. Hardenability increases as austenitizing temperature increases. The optimum time at austenitizing temperature is from 10 to 30 minutes. Preheating is unusual except for very large tools or those with intricate cross sections.
The graph shows the maximum section thicknesses of three classes of water-hardening tool steels that develop minimum hardness of 60 HRC when oil quenched from various austenitizing temperatures.
It is particularly important to protect shallow-hardening steels against scaling and decarburization. Severe scaling can interfere with heat transfer during quenching and slow the required high rate of cooling. Decarburization will produce a soft surface on any tool steel, but in a deep-hardening steel it can be ground off until the underlying hard high-carbon area is reached. Grinding a shallow-hardening steel will frequently expose the soft core.
Volume 4D, Heat Treating of Irons and Steels -> Tool steels -> Introduction to Heat Treating of Tool Steels -> Water Hardening Tool Steels