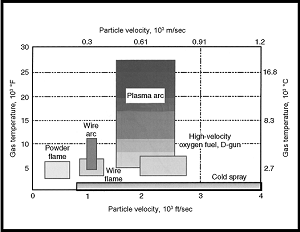
The diagram compares the particle velocity and gas temperature ranges of cold spray and other thermal spray processes: In the cold spray process, the gas and particle temperatures are much lower and the gas and particle velocity are much higher than in other thermal spray processes.
There typically are four regions of particle/substrate interactions that can be defined by particle velocity. In the first region, the particle velocity (Vp) is too low for a given coating/substrate combination to form a coating, and the feedstock particles are reflected from or bounce off the surface and do not form a contiguous coating or deposit.
When the particles impinge at moderate velocities, solid particle erosion of the substrate surface occurs, but no coating is deposited.
When the particles reach a critical velocity (Vcrit), the particles begin to plastically deform, adhere to the substrate, and form a coating. The critical velocity varies with particle and substrate material. As Vp increases, the particles undergo more deformation, typically leading to higher coating densities. At very high velocities, the solid particles start to erode the surface of the substrate. When this occurs, the particle velocity is called the erosion velocity (Verosion).
https://dl.asminternational.org/books/book/12/chapter/133714/Cold-Spray-Process