P20 mold steel is seldom carburized for molds used in compression molding, particularly for molding the more abrasive plastics. Carburizing temperatures no higher than 1650°F are recommended for this steel because higher temperatures may impair polishability; otherwise, conventional carburizing practice is used, and molds may be quenched in oil directly from the carburizing temperature. A common working range is 54 to 58 HRC.
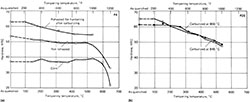
The graph shows tempering characteristics of carburized mold steels.
(a) Upper curve represents steel carburized in hardwood charcoal 1675 to 1700°F for 8 hours, air cooled in pack, reheated at 1725 to 1750°F, cooled in air, and tempered. Middle curve represents steel carburized in cast iron chips at 1725 to 1750°F, removed from pack, cooled in air, and tempered.
(b) Surface hardness after heating at temperature for 2 hours in carburizing compound, followed by oil quenching and tempering.
Volume 4D, Heat Treating of Irons and Steels ⇒ Tool Steels ⇒ Heat Treating of Mold Steels and Corrosion-Resistant Tool Steels ⇒ Recommended Heat Treating Practices