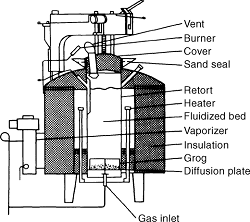
 The indirectly heated fluidized-bed furnace is heated electrically though a fluidized-bed furnace may also be gas heated. Fluidized beds have been designed to perform a wide variety of heat treating tasks including stress relieving, preheating, hardening, quenching, annealing, and tempering, as well as a variety of surface treatments such as carburizing, nitriding, and steam tempering.
However, despite their numerous advantages, these furnace types were not really accepted in the market. In the early 1980s, this furnace technology seemed to be on the right track as an alternative to salt bath technology, showing similar advantages and applications but without the environmental hazard of salt compounds, waste disposal, recycling of salts, and so on. Nowadays it can be concluded that salt bath technology was partially substituted by vacuum technology, but especially for bainitic hardening (austempering processes), salt baths are still commonly used and show a slightly growing tendency, whereas fluidized beds are hardly used any more.
Most fluidized-bed furnaces are used at temperatures below 1095 °C (2000 °F), although some manufacturers have furnaces capable of treating components to temperatures through 1205 °C (2200 °F). This temperature limitation is related to the wear and tear on the retort materials at high temperatures, which was one of the reasons for the reduced interest in this furnace type after the initial hype.
For more information, click on the link below (subscription required). Then scroll to Figure 8.
R. Schneider ; R. Mesquita ; H. Altena ; T. Müller ; P. Seemann,Processes and Furnace Equipment for Heat Treating of Tool Steels, ASM International, 2014, https://doi.org/10.31399/asm.hb.v04d.a0005958